
Automatic CNC Laser Machines: From Entry-Level To Professional
Last Updated: 2026-10-28 10:37:25
Throughout the last few years, automatic CNC laser machining has become widespread, expanding from hobby shops to small businesses, schools, as well as strictly industrial manufacturers. Increased competition on the market also means that choosing the right CNC laser machine for cutting, engraving, marking, etching, cleaning and welding will be harder than ever. Most guys have no idea where to start. STYLECNC would like to assist you throughout the selection process, not by suggesting any specific CNC laser kit, but rather by guiding you to make your own decision, in accordance with your needs and budget. There's a lot to know before you can find the right CNC laser cutter, engraver, marker, etcher, cleaner and welder to start or grow your business. In order to help you get the right information, here are some of the CNC & laser basics you need to know. This guide will discuss what you need to consider when determining which CNC laser machine is the best kit for your business.
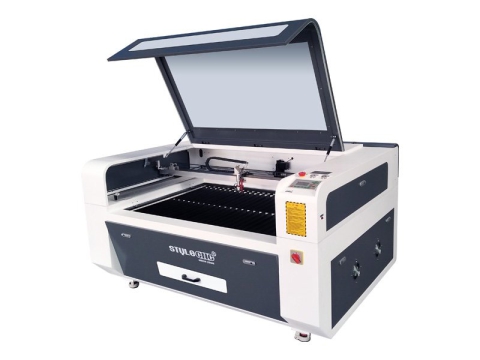
STJ1390
$3,500 - $5,500
Cheap CO2 Laser Engraver 60W, 80W, 100W, 130W, 150W, 180W
Cheap CO2 laser engraving machine with 60W, 80W, 100W, 130W, 150W,180W power options is used for wood, fabric, leather, glass, acrylic, paper, plastic, stone.
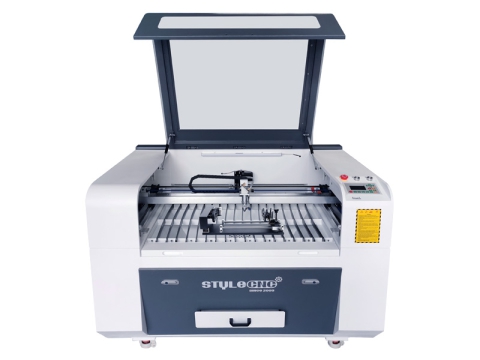
STJ9060
$2,600 - $3,600
2026 Best Entry Level Small Laser Engraver for Beginners
2026 best small laser engraver is an entry level mini laser engraving machine with compact structure for beginners to engrave and cut crafts, arts, gifts.
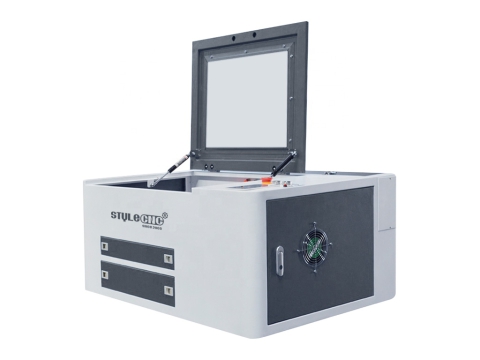
STJ6040
$2,400 - $2,600
Budget-Friendly Small Desktop Laser Engraver Cutter Machine
Small desktop laser engraver cutter machine with 40W/60W CO2 laser tube is an affordable hobby laser with a compact design for home use and small business.
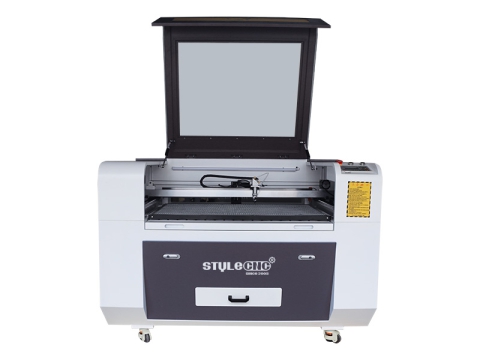
STJ9060
$2,600 - $3,600
2026 Top Rated Laser Wood Engraving Machine for Sale
Looking for the best wood laser engraving machine to cut, etch, engrave wood, plywood, MDF? Review 2026 top rated laser wood engraver for sale at cost price.
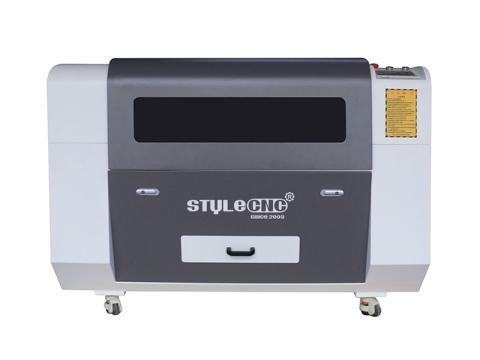
STJ9060
$2,600 - $3,600
Hobby Laser Engraver for Plastic, Acrylic, Glass, Polymer
STJ9060 hobby laser engraver with 2x3 table top to cut & engrave plastic, acrylic, glass, rubber, polymer, wood for hobbyists, small business, and home shop.

STJ1390-2
$3,800 - $6,500
Affordable Laser Engraver for Leather, Fabric, Paper, Jeans
Affordable laser engraver with CO2 laser tube is designed for cutting, etching & engraving leather, fabric, textile, paper, cardboard, jeans, and fibers.
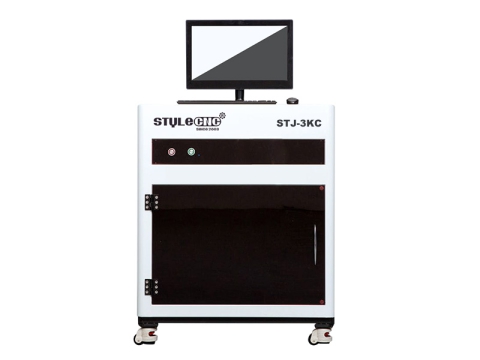
STJ-3KC
$15,000 - $18,000
2026 Best 3D Laser Crystal Engraving Machine for Sale
3D subsurface laser crystal engraving machine is 2026 best engraver to create personalized bubblegram, gift, souvenir, art, craft, trophy with crystal & glass.
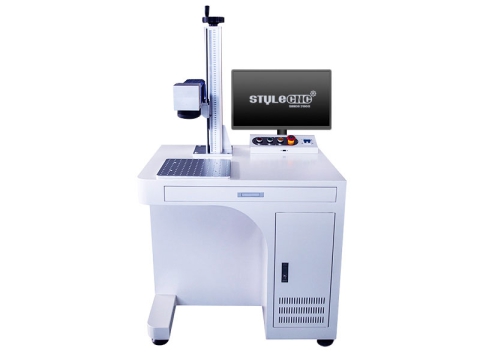
STJ-50F-D
$2,400 - $4,200
50W Fiber Laser Deep Engraving Machine for Metal
Laser deep engraving machine with 50 watt fiber laser source is the best metal laser engraver for relief etching and marking, as well as thin metals cutting.
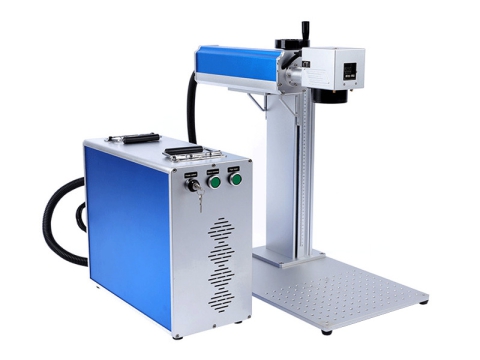
STJ-50F-S
$2,400 - $6,500
2026 Best Laser Engraver for Gun Stippling & Grip Texturing
2026 best budget laser engraving machine for gun stippling & grip texturing with IPG fiber laser generator for 2D/3D color engraving or deep engraving on guns.
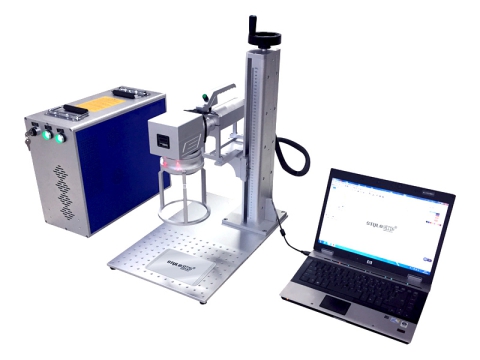
STJ-30F-H
$1,400 - $2,500
Mini Handheld Fiber Laser Marking Machine 20W, 30W, 50W
Mini handheld fiber laser marking machine with 20W, 30W, 50W, 100W power options is compact and portable for fine engraving anywhere indoors and outdoors.
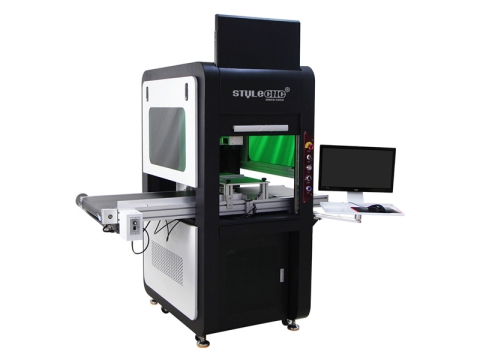
STJ-50F-C
$6,200 - $9,000
Laser Marking Machine with CCD Visual Positioning System
The best fiber laser marking machine with CCD visual positioning system is used for mass production at low cost with diversified & complex engravings and cuts.
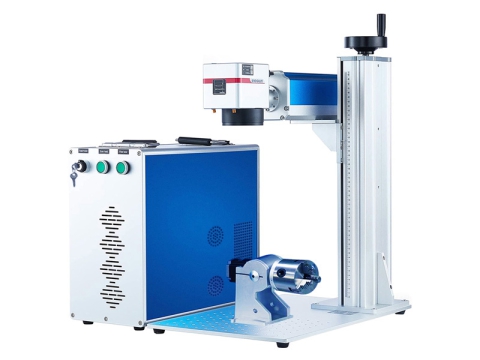
STJ-30FM-S
$2,500 - $5,800
Affordable Fiber Laser Engraving Machine for Color Marking
Affordable fiber laser engraver for color marking is designed to etch black, white, grey, and colors on metals of stainless steel, titanium, and chromium.
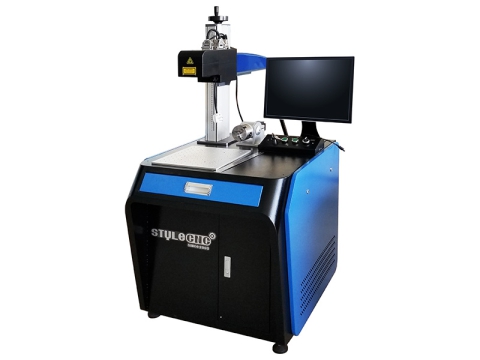
STJ-100FM-3D
$6,800 - $8,800
3D Fiber Laser Marking Machine for Metal Texturing
3D fiber laser marking machine is a 5-axis laser texturing system for etching on 3D curved metal surfaces and deep engraving textures & reliefs on metal molds.
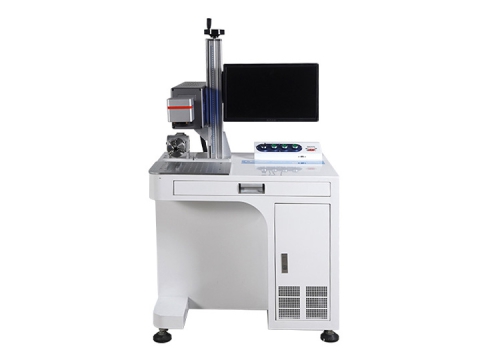
STJ-30C
$4,000 - $6,500
CO2 Laser Marking Machine for Glass, Acrylic, Plastic
2022 best CO2 laser marking machine is used for engraving plastic, acrylic, glass. Now the affordable CO2 desktop laser marking system for sale at cost price.
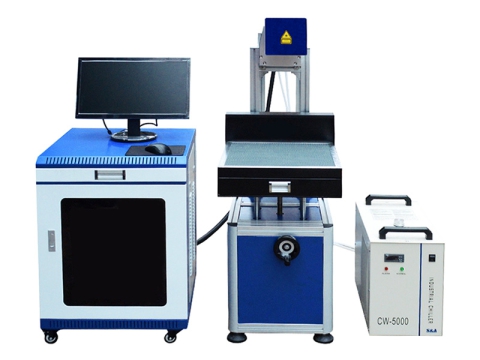
STJ-80C
$4,700 - $5,500
Low Cost CO2 Laser Marking Machine for Leather & Fabric
Low cost CO2 laser marking machine is used for personalizing leather, fabric, jeans, textile. Now the cheap CO2 laser marker system for sale at cost price.
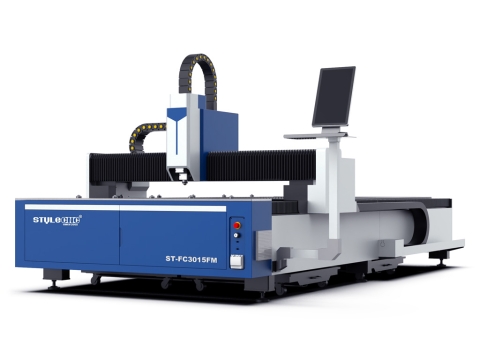
ST-FC3015FM
$15,000 - $43,000
2026 Best Sheet Metal Laser Cutter for Sale (1500W - 6000W)
2026 best sheet metal laser cutter is a full-size automatic CNC laser metal cutting machine with 1500W to 6000W power options for parts, signs, arts and crafts.
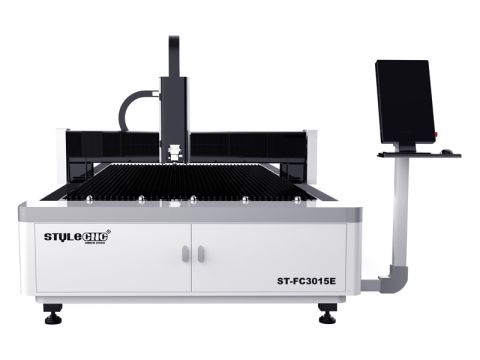
ST-FC3015E
$12,800 - $16,000
2026 Top Rated Fiber Laser Cutting Machine for Sale - 2000W
The most popular and top-rated fiber laser cutting machine for metal fabrication is available at an affordable price with power options of 1500W, 2000W, 3000W.
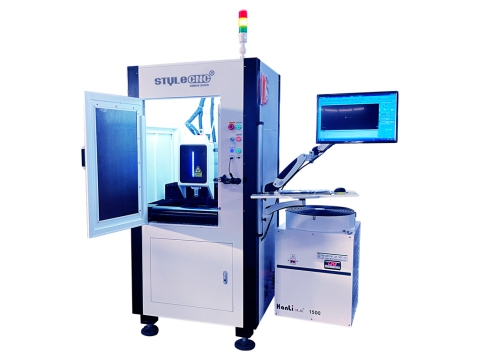
ST-FC3030
$12,200 - $14,500
Mini Laser Metal Jewelry Cutter for Silver, Gold, Copper
Looking for a precision laser cutter to make metal jewelry with silver, gold, copper, stainless steel? Review the mini compact laser jewelry cutter for sale.
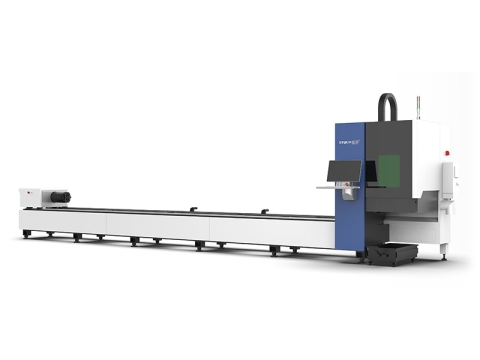
ST-FC6020T
$20,800 - $56,800
2026 Top Rated Fiber Laser Tube Cutting Machine for Sale
2026 best fiber laser tube cutting machine is an auto CNC metal pipe cutter used to create shapes & contours on square, round, rectangular, oval, shaped tubes.
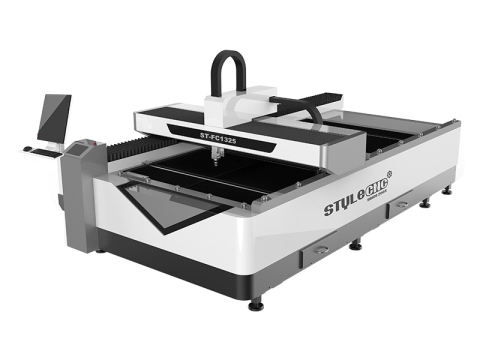
ST-FC1325
$14,000 - $18,500
2026 Cheapest 4x8 Fiber Laser Stainless Steel Cutter 1500W
2026 cheapest 4x8 laser stainless steel cutting machine with 1500W fiber laser can cut metals less than 2mm aluminum, 3-4mm stainless steel, 12mm carbon steel.
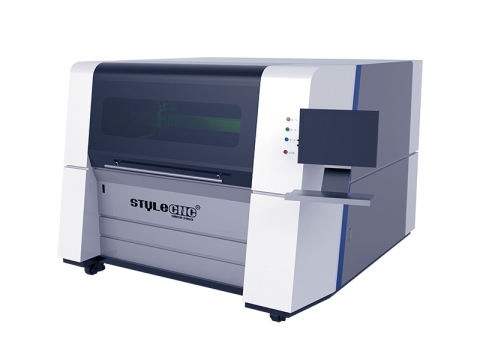
ST-FC1390
$17,000 - $31,000
Entry Level Small Metal Laser Cutter for Beginners
ST-FC1390 small metal laser cutter with fiber laser generator is a compact entry level fiber laser cutting system for hobbyists and home use in small business.
ST-18R
$46,000 - $78,000
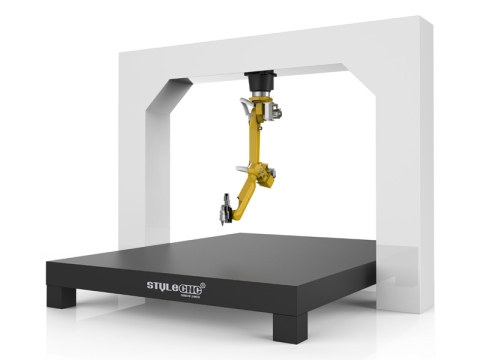
Industrial 3D Robotic Fiber Laser Cutting Machine for Metal
Industrial 3D robotic fiber laser cutting machine with 5 axis robot arm for 3D curved metal parts, metal tubes, auto parts, kitchenware, electronic components.
ST-FC3015GAR
$40,000 - $730,000
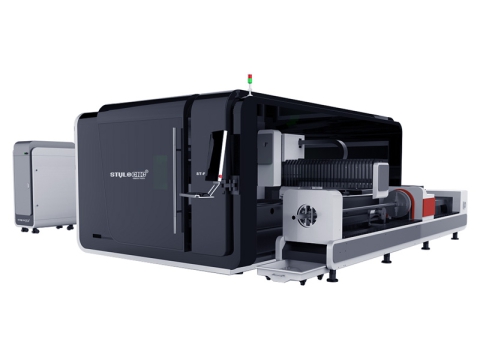
Dual-Purpose 6kW Fiber Laser Cutter for Metal Sheet & Tube
Dual-purpose 6000W fiber laser cutting machine for sale at affordable price with dual functions to cut sheet metals, metal plates, metal tube, and metal pipes.
ST-FC3015LR
$19,800 - $46,000
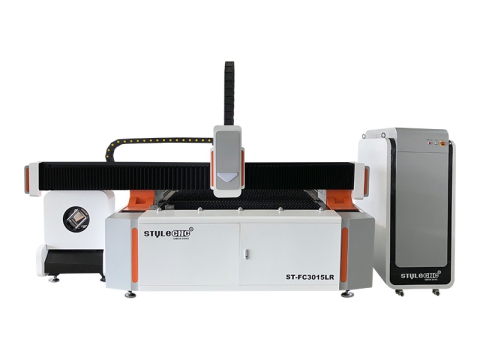
5x10 Industrial Fiber Laser Metal Cutting Machine for Sale
Affordable 5x10 industrial fiber laser metal cutting machine for sale at cost price to cut both sheet metals and tubes all in one machine for metal fabrication.
STJ1390
$2,850 - $10,000
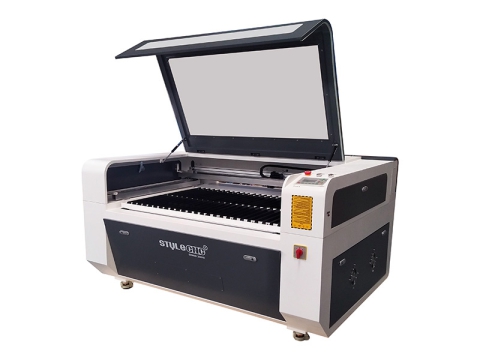
2026 Best CO2 Laser Cutter for Small Business and Home Use
2026 best CO2 laser cutter is designed for small businesses, home users, and hobbyists to engrave and cut wood, paper, acrylic, plastic, glass, leather, fabric.
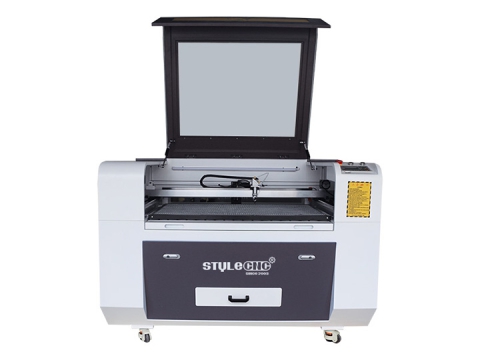
STJ9060
$2,800 - $4,000
Entry Level CO2 Hobby Laser Cutter Machine for Beginners
CO2 hobby laser cutter machine for beginners is an entry-level laser engraving & cutting system with 2x3 table kits for hobbyists, small business, home shop.
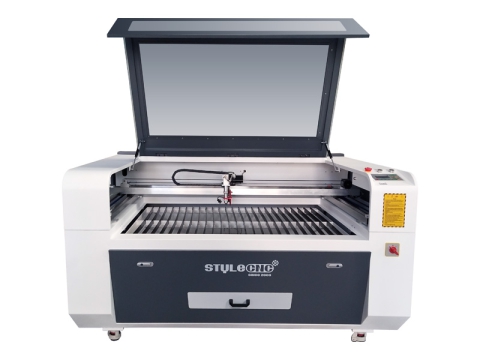
STJ1390
$3,500 - $10,000
100W Laser Wood Cutter Engraving Machine for Woodworking
100W laser wood cutter engraving machine is an affordable CO2 laser cutter kit for newbies and beginners to engrave and cut hardwood, plywood, MDF, bamboo.
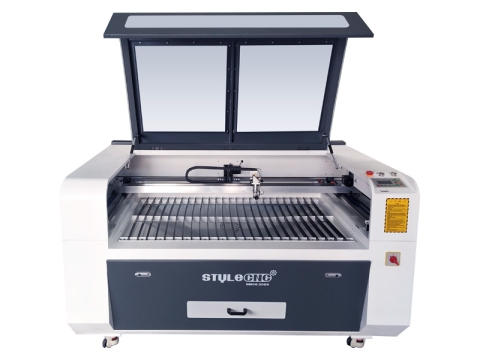
STJ1610
$3,200 - $12,000
2026 Best Acrylic Laser Cutting Machine for Sale
2026 best acrylic laser cutting machine is used to cut plastics, clear and colored acrylic sheets as letters, numbers, signs, logos, patterns, arts and crafts.
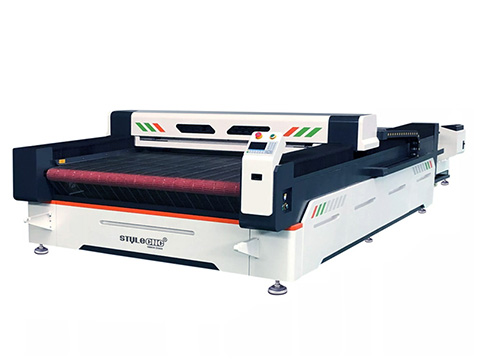
STJ1630A
$9,800 - $10,800
2026 Best Industrial Fabric Laser Cutting Machine for Sale
2026 best industrial fabric laser cutting machine with large conveyor table and automatic feeding system for clothing, garment, fashion in commercial use.
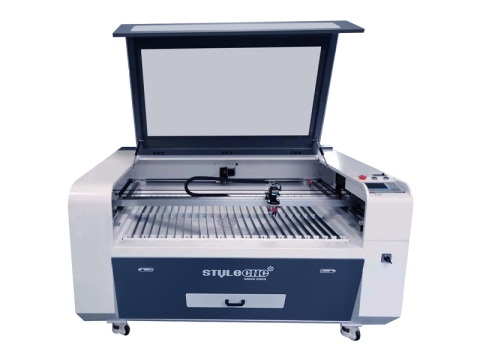
STJ1610-CCD
$4,500 - $12,700
CNC Laser Cutter With CCD Camera Visual Recognition System
CNC laser cutter integrates a CCD camera visual recognition system, ideal for crafting intricate embroidered badges from fabrics such as premium fabric, canvas, and cotton twill.
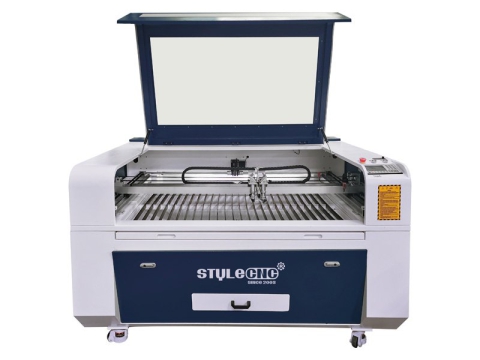
STJ1390-2
$4,200 - $11,000
Dual-Head CO2 Laser Cutter for Paper and Cardboard
Dual head CO2 laser cutter comes with two laser cutting heads to cut paper and cardboard for creating personalized invitations, cards, mockups, storage boxes.
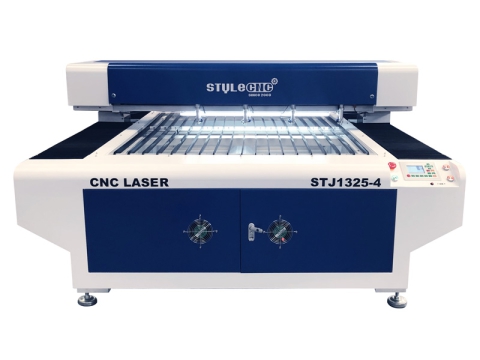
STJ1325-4
$8,400 - $20,000
2026 Best-Selling 4x8 Laser Cutter for Plywood & MDF
2026 best-selling affordable 4x8 laser cutter with four laser heads can cut full sheet plywood, MDF to make multiple projects from 1 up to 4 at the same time.
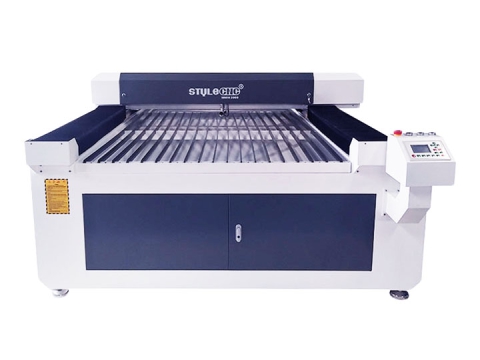
STJ1325
$5,200 - $10,800
2026 Best Industrial Laser Foam Cutting Machine for Sale
2026 best industrial laser foam cutting machine is used to cut EVA foam, EPS foam, XPS foam, Styrofoam, PE foam, rubber for making custom foam projects & plans.
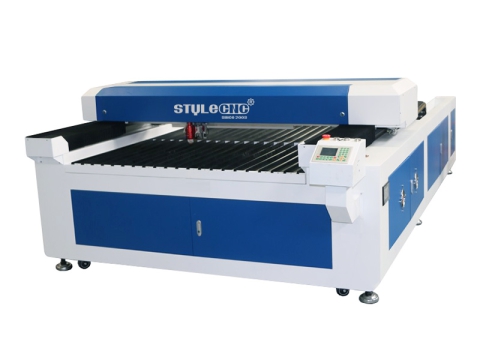
STJ1325M
$6,500 - $13,000
Metal & Nonmetal Laser Cutter with 300W CO2 Laser Tube
Metal & nonmetal laser cutting machine with 300W CO2 laser tube is a new designed laser cutter for stainless steel, alloy, acrylic, leather, plywood, MDF, wood.
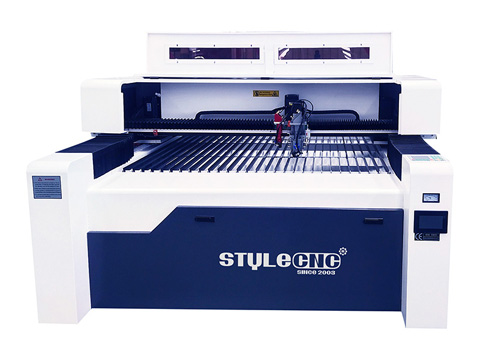
STJ1325M-2
$9,000 - $14,000
Versatile 4x8 CNC Laser Engraving Cutting Machine for Sale
4x8 CNC laser engraving cutting machine is used to engrave and cut both metals—such as steel, aluminum, brass—and nonmetals, including acrylic and plywood.
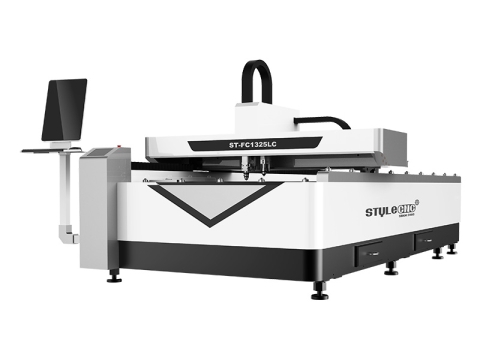
ST-FC1325LC
$15,800 - $20,500
Fiber & CO2 Combo Laser Cutting System for Metal & Nonmetal
1500W fiber laser metal cutting machine combined with 150W CO2 laser cutting system is a hybrid laser cutter for metal, wood, acrylic, plastic, leather, fabric.
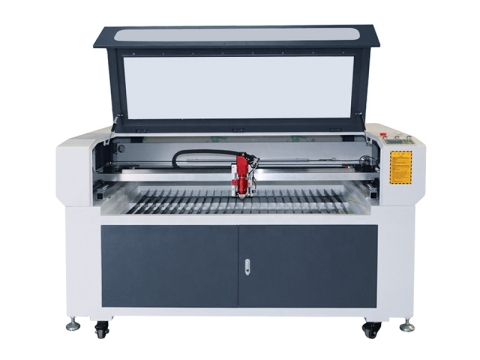
STJ1610M
$7,500 - $12,000
2026 Best Metal & Nonmetal Laser Cutting Machine for Sale
2026 best mixed hybrid laser cutting machine STJ1610M adopts CO2 sealed laser tube, which can cut thicker nonmetals, and metal materials from 0.5mm up to 2mm.
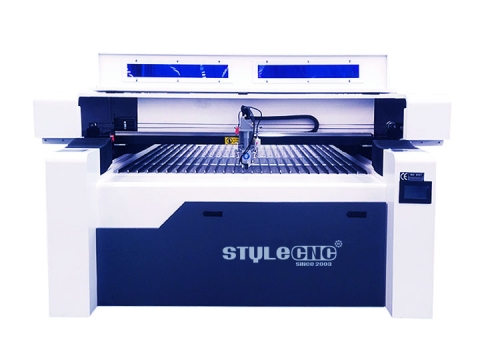
STJ1325M
$8,000 - $12,800
Mixed CNC Laser Cutter Engraving Machine for Wood & Metal
Mixed CNC laser cutter engraving machine is a versatile hybrid laser that can engrave and cut various materials from non-metals like wood to metals like steel.
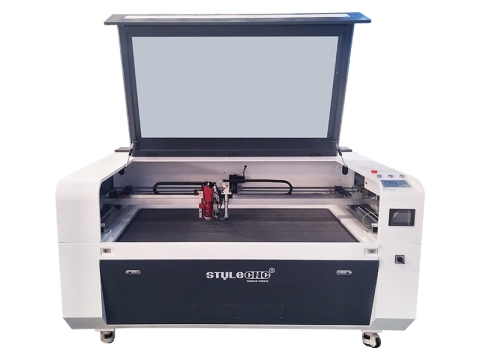
STJ1390M-2
$7,500 - $12,500
Profitable Mixed CNC Laser Cutter Hybrid Cutting Machine
Profitable mixed CNC laser cutter hybrid cutting machine is a beneficial laser cutting system for wood, plywood, MDF, acrylic, and metals in commercial use.
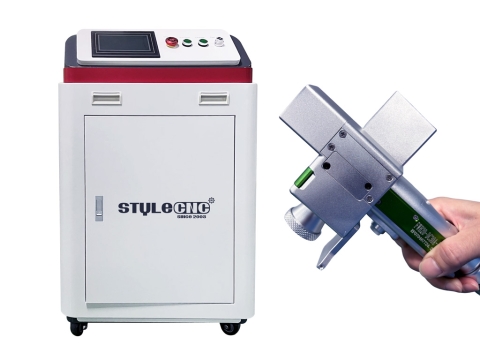
LC3000
$3,800 - $6,000
2026 Best Handheld Fiber Laser Cleaning Machine for Sale
2026 best handheld fiber laser cleaning machine is a manual portable laser cleaner with fiber lasers for rust removal, paint stripping, and coating removal.
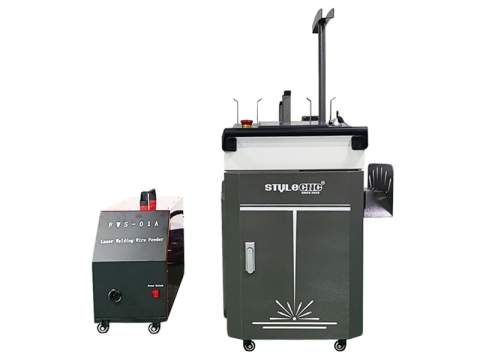
LCW1500
$3,300 - $4,700
3-In-1 Handheld Laser Welding, Cleaning, Cutting Machine
3-in-1 laser welder, cleaner, cutter is a portable all-in-one laser machine with handheld laser gun for cutting & welding metal, cleaning rust, paint, coating.

LCW3000
$3,600 - $16,800
2026 Best Portable Handheld Laser Welding Machine for Sale
2026 best portable laser welding machine comes with 1500W, 2000W, 3000W, 6000W handheld fiber laser welder gun for metal joints of edge, butt, tee, corner, lap.
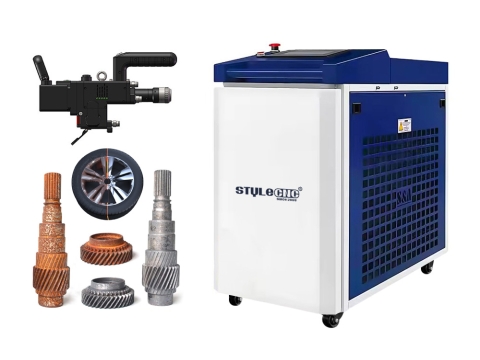
LC6000
$12,500 - $13,500
2026 Best Handheld Laser Rust Removal Machine for Sale
2026 best handheld laser rust removal machine is a portable laser cleaner used to take rust off metals with fiber laser powers of 1500W, 2000W, 3000W, 6000W.
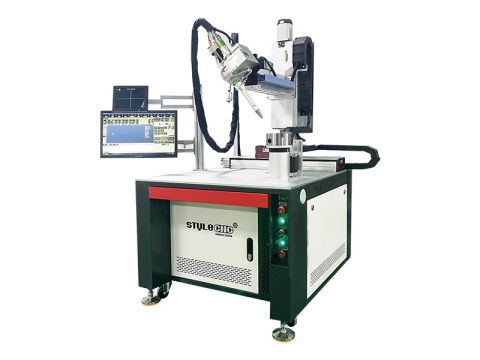
LWT2000
$8,800 - $11,300
Hi-Precision Automatic CNC Laser Welding Machine for Sale
CNC laser welding machine is an automatic laser welder with fiber laser beam welding system for precision metal joints of butt, lap, corner, tee, edge, flange.
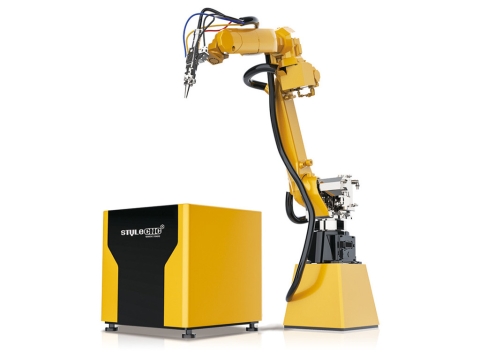
LWR3000
$10,800 - $32,000
Automatic Smart 3D Industrial Laser Welding Robot for Sale
Find & buy automatic 3D fiber laser welding robot at cost price with 6-axis industrial robotic arm from popular welding machine manufacturers and brands.
Feature Stories & Articles That Interest You



Find & Buy Your First CNC Laser Machine
Definition
A CNC laser machine is an automated manufacturing tool that utilizes fiber, carbon dioxide (CO2), or ultraviolet (UV) laser beams to mark, etch, engrave, and cut both metallic and non-metallic materials, weld metal components, and remove contaminants, rust, paint, or coatings. The equipment consists of a machine bed, controller, power supply, laser generator, laser tube, processing head, mirrors, lenses, water chiller, stepper or servo motors, air compressor, gas cylinders, air storage tank, dust collector, air-cooling filter, and dryer, along with supporting software and systems. These machines are widely applied across various sectors, including industrial manufacturing, education, small businesses, home workshops, advertising, arts and crafts, gifts, toys, packaging, printing, leather processing, apparel, automotive manufacturing, musical instrument production, construction, label making, and the medical field.
Applications
CNC (Computer Numerical Control) laser machines are used for marking, etching, engraving, cutting, welding, and cleaning a wide variety of metallic and non-metallic materials:
Metallic Materials: Carbon steel, stainless steel, tool steel, spring steel, galvanized steel, aluminum, copper, gold, silver, alloys, titanium, iron, brass, manganese, chromium, nickel, cobalt, and lead.
Non-Metallic Materials: Wood, medium-density fiberboard (MDF), plywood, particleboard, acrylic, plastics, polymethyl methacrylate (PMMA), leather, fabrics, cardboard, paper, rubber, Depron foam, EPM, Gatorfoam, polyester (PES), polyethylene (PE), polyurethane (PUR), neoprene, textiles, bamboo, ivory, carbon fiber, polyvinyl chloride (PVC), polyvinyl butyral (PVB), polytetrafluoroethylene (PTFE/Teflon), and beryllium oxide, as well as any materials containing halogens (chlorine, fluorine, iodine, astatine, or bromine), phenolic resins, or epoxy resins.
Types
CNC laser machines are categorized into cutting, engraving, marking, cleaning, and welding machines.
Cutters include fiber, CO2 and hybrid laser cutters,
Engravers include fiber, UV and CO2 laser engraver.
Markers include fiber, CO2 and UV laser marking machine.
Welders include handheld and automatic laser welding machine.
Technical Parameters - Specifications
| Brand | STYLECNC |
| Laser Power | 20 Watts - 60000 Watts |
| Laser Wavelength | 10.6 μm, 1064 nm, 355 nm |
| Laser Type | Fiber, CO2 and UV laser |
| Capability | Cutting, Engraving, Etching, Marking, Cleaning, Welding |
| Price Range | $2,400 - $260,000 |
Cost & Pricing
The cost structure of a CNC laser machine includes various components (such as CNC controllers, power supplies, laser generators, laser heads, laser tubes, lenses, mirrors, machine frames, water chillers, stepper or servo motors, dust collection systems, air compressors, gas cylinders, air storage tanks, air-cooling filters, and dryers), as well as software and control systems, transportation costs, taxes, customs clearance fees, and services and technical support.
The price range for CNC laser cutting machines is between $2,600 and $300,000; CNC laser engraving machines range from $2,400 up to $70,000; CNC laser marking machines cost between $3,000 and $70,000; and CNC laser welding machines range from $16,800 to $28,000. Overall, by 2026, the average cost to purchase a piece of CNC laser equipment is expected to be approximately $6,000.
Benefits and Advantages
As a modern technological advancement, CNC (Computer Numerical Control) laser processing machines direct a high-energy-density laser beam onto a workpiece. This causes localized heating and melting, after which high-pressure gas blows away the molten material—enabling precise cutting (shaping or contouring) or engraving (of text and patterns).
• Features narrow kerf widths, high precision, and excellent surface finish, eliminating the need for secondary processing.
• Offers a high degree of automation and supports fully enclosed operation; it is clean, quiet, and significantly improves the working environment for operators.
• Lowers processing costs. While the initial investment in equipment is substantial, the cost per unit decreases significantly through continuous, large-scale production.
• Employs a non-contact processing method with low inertia, resulting in high processing speeds. When integrated with CAD/CAM software via a CNC system, it offers convenient, time-saving operation and exceptional overall efficiency.
• The high energy density of the laser beam can melt any metal, making it particularly effective for processing challenging materials—such as those with high hardness, high brittleness, or high melting points.
• Characterized by short interaction times and a small heat-affected zone (HAZ), which minimizes thermal deformation and internal stress. Furthermore, because it is a non-mechanical contact process, the workpiece remains free from mechanical stress, making it ideal for precision machining.
• As a computer-based system, CNC laser technology allows for flexible adjustments and modifications. This makes it highly suitable for customized production—especially for sheet metal components with complex contours and shapes. In scenarios involving variable batch sizes or short product lifecycles, traditional mold manufacturing is often neither cost-effective nor time-efficient; in such cases, laser cutting and engraving offer a clear advantage.
A CNC laser machine is not merely a consumer product, but a powerful tool for wealth creation. Since the primary purpose of acquiring such equipment is to boost production capacity, enhance efficiency, reduce costs, and elevate technical capabilities, selecting the right machine is of critical importance.
How To Use?
Step 1. Determine the production plan based on the production schedule and distribute the processing drawings to the equipment operation team.
Step 2. Draftsmen analyze the drawings according to the plan and use CAD software to create the necessary technical drawings.
Step 3. A quality inspector verifies and confirms the accuracy of the drawings prepared by the draftsmen.
Step 4. The production supervisor calculates the estimated completion time based on the digital drawings and prepares the required materials and auxiliary cutting gases.
Step 5. Programmers use specialized software to generate NC (numerical control) machining program files.
Step 6. The supervisor issues a task order to the equipment operators (the task order includes: program name, material type, material thickness, maximum dimensions of the workpiece, and the required quantity).
Step 7. Perform a trial cut of the first piece and submit it to a quality inspector for verification. Once the dimensions are confirmed to be within specifications, archive the first piece.
Step 8. Begin batch processing.
Step 9. Assign identification numbers to the finished workpieces.
Precautions
Startup Precautions
• Inspect the work table and check for any obstructions that might hinder the X, Y, and Z axes from returning to their home (zero) positions. If any such obstructions are found, please remove them.
• Prepare the necessary gases for cutting and adjust their pressures to the required levels. For example, oxygen pressure for cutting should be set to 0.4–0.5 MPa, and nitrogen pressure to 1.8–2.2 MPa. (Note: Pressure should be adjusted based on the thickness of the material being cut—use lower pressure for thin sheets and higher pressure for thick plates.)
• Open the drain valve on the air compressor’s storage tank to remove accumulated water and impurities, then close the valve and start the air compressor. (The loading and unloading pressures for the air compressor should be set to 0.8 MPa and 1 MPa, respectively.)
• Turn on the voltage stabilizer (set the output voltage to between 380 V and 400 V).
• Turn on the air dryer (which cools and dries the gas produced by the air compressor before delivering it to the mirrors).
• Turn on the water chiller, verify that the water level and pressure are within the normal range, and activate the cooling water and ambient-temperature water supplies. The cooling water pressure should be set to approximately 0.5 MPa, with an upper temperature limit of 20°C. The ambient-temperature water pressure should be approximately 0.3 MPa, with an upper temperature limit of 30°C in the summer and 25°C during other seasons.
• Ensure that the supply pressures for high-purity nitrogen (purity ≥99.999%), high-purity carbon dioxide (purity ≥99.999%), and high-purity helium (purity ≥99.999%) are all above 0.4 MPa.
• Turn on the laser generator.
• Power on the equipment and log into the operator system (password: "user"). Release the emergency stop button and clear any alarms. Perform the "return to reference point" (homing/SET ZERO) procedure. Activate the CLC button, then press the start button (LASER ON). Once "HV READY" appears on the electrical control cabinet panel, you may press the "HV ON" button on the CNC control panel.
• Input the required machining program into the CNC system according to the production schedule, and proceed with the machining process.
Shutdown Precautions
• Return the X, Y, and Z axes to their reference points.
• Turn off the high-voltage switch (HV ON).
• Turn off the power (LASER OFF).
• Press the emergency stop button to shut down the CNC panel. (Do not force a power cut to the CNC panel; an improper shutdown may result in the loss of system data.)
• Disconnect the power supply to the machine tool’s electrical control cabinet.
• Stop the chiller and disconnect its power supply.
• Disconnect the power supply to the electrical control cabinet.
• Stop the air compressor and disconnect its power supply.
• Stop the condenser and disconnect its power supply.
• Close all auxiliary gas valves.
• Clean the CNC laser machine.
Precautions During Operation
• Prevent the formation of dross during the piercing process (by using a protective lens).
• When cutting materials such as stainless steel, galvanized sheets, or aluminum, dross can easily form and contaminate the focusing lens. To avoid such issues caused by improper parameter settings, please observe the following guidelines:
• Set the piercing height to 2–5 mm; increase this height for thicker materials.
• For materials with a thickness of 2.5 mm or greater, enable the "cut small holes after piercing" function and set the small-hole radius to 0.5–1 mm.
• For stainless steel 3 mm thick or less, nitrogen must be used for piercing.
• For stainless steel thicker than 3 mm, either nitrogen or oxygen may be used for piercing.
• For aluminum or galvanized sheets, oxygen must be used for piercing.
• When using oxygen for piercing, enable the "wait for oxygen/nitrogen switch" function and set the switching time to 1–3 seconds.
• During the cutting process, closely monitor the material for deformation. If the sheet warps or vibrates (bounces), flatten it before cutting to prevent incomplete cuts or the formation of dross caused by such movement.
Personal Safety Tips
• Identify the nature of the material to be cut, determine whether it will release toxic gases during the cutting process, and ensure that an adequate smoke/fume extraction system is in place. (Note: Operators must wear protective equipment.)
• Pay close attention to the instructions provided in the equipment operation manual.
Machining Safety Tips
• Before beginning machining operations, please observe the following: verify the properties of the material to be cut, understand how it reflects the laser beam, and ensure it has sufficient light-absorption capacity to prevent reflected light from damaging the laser source.
• During operation, take precautions against electrical hazards and potential laser-related injuries.
Electricity Safety
The equipment is powered by 390–400V AC, which is stepped up to a high voltage of over 10kV via a high-voltage transformer to provide the necessary excitation energy.
• Do not open the electrical cabinet or the protective doors of the laser head while the equipment is powered on, as this poses a risk of electric shock.
• Even after the equipment has been powered off, do not open the electrical cabinet or the protective doors of the laser head (especially the rear door of the electrical cabinet).
• This is because residual electrical charge may still be present within the laser system, which could easily cause injury to personnel.
Laser Safety
A laser is a form of invisible light with high power density, capable of causing burns and radiation-related injuries to the human body. When using a laser, do not stand in the path of the beam, as this may result in burns; never look directly into the laser, as doing so can cause injury. It is recommended to wear protective eyewear while operating the device.
Focusing Lenses Precautions
Pay attention to the cleanliness of the focusing lens and clean it regularly. If any deviation in the optical path is detected, it must be adjusted on a monthly basis. Furthermore, perform routine maintenance on the equipment in accordance with the requirements outlined in the operation manual to ensure it consistently remains in optimal operating condition.
Cold Dryer Precautions
• The indoor temperature must not exceed 35°C.
• Drain wastewater daily.
• Clean the air vents once a week (using an air gun).
• Clean the filters once a month (using a soft brush and soapy water).
Maintenance & Troubleshooting
Machine Tool Daily Maintenance
• Inspect the external optical path every 1 to 2 months. If the copper mirrors are found to be contaminated, clean them promptly (following standard operating procedures). After cleaning, the external optical path must be realigned; once aligned, do not move any components.
• Lubricate and maintain the lead screws and linear guides every 2 weeks to 1 month.
• Clean the entire machine surface once a week.
• Remove dust from the chiller’s radiator once a week (you may use an air stream to blow through the radiator). Check the water level in the chiller monthly and top it up as needed (ensure the water used is as clean as possible).
• Inspect the refrigerated air dryer filter every 2 to 3 months and clean the filter element (using alcohol). Apply gentle pressure when cleaning; if there is oily residue, use gasoline to clean it. Replace the filter element if it is damaged.
• Clean the guide rails of the worktable and the lifting platform once a month.
• Check the chiller monthly. If the water level is low, add water. Pure water should be replaced every 2 months, and distilled water every 6 months. If the water quality appears poor during inspection, replace it immediately.
• When cutting carbon steel thicker than 9.6 mm or stainless steel thicker than 5 mm, it is recommended to use a long-focal-length lens to better protect the lens.
• Always clean the lens after cutting stainless steel, wood, rubber, organic glass (acrylic), or quartz materials.
• During the summer, when temperatures are high, the Z-axis and its housing may become slightly warm during prolonged operation of the CNC laser equipment; this is normal. However, if the temperature becomes excessively high—to the point of being hot to the touch—it is abnormal. In such cases, check the following:
- Ensure that the control switch for the external optical path on the chiller is turned on.
- Verify that the Z-axis optical path is properly aligned.
- Check the surface of the focusing lens for significant damage (e.g., the presence of numerous spots).
- Ensure that the Z-axis is positioned vertically. - Check whether the two copper mirrors located near the Y-axis are clean. Any of the aforementioned issues may cause the Z-axis and its housing to heat up; please remain vigilant during subsequent operations.
- After replacing the gas mixture, ensure the gas mixture valve is tightened, then gently close the cover panel.
• Always follow proper operating procedures. When executing the "RETRACT" command followed by "CYCLE START," or the "SET TO CUT" command followed by "CYCLE START," pay close attention to the program display. Never initiate rapid movement while the cutting head is descending (doing so carries a high risk of causing a collision).
• The following conditions can lead to frequent "piercing blowouts" (which can damage the lenses):
- Unstable laser pulses, potentially caused by fluctuating operating voltage or other factors.
- Misalignment of the optical path.
- Improper piercing parameter settings.
• Periodically clean the interior of the Z-axis assembly using a cotton swab or absorbent cotton dampened with a small amount of acetone.
CNC Laser Daily Maintenance
To ensure that a CNC laser machine achieves and maintains optimal performance, it must be provided with a suitable operating environment—specifically, one that meets all requirements regarding water, gas, and electrical supply.
The primary function of the cooling water is to dissipate heat generated during the machine's operation, preventing it from running at excessively high temperatures. A chiller circulates cooling water to remove heat from the electrical cabinet and the resonant cavity, thereby ensuring the equipment functions correctly. The cooling water temperature should be maintained at 20°C. Because the cooling water flows through the chiller’s piping and the copper plates within the resonant cavity, there are strict requirements for the water’s pH level and electrical conductivity. If the water quality is substandard, long-term use can damage the laser. To prevent such issues, anti-corrosion agents must be added to the water, and the electrical conductivity should be monitored regularly to ensure it remains within the required specifications. The radio-frequency (RF) generator is cooled using deionized water, which also requires the addition of specific agents to ensure its electrical conductivity meets the prescribed standards.
Operating gases fall into two categories: a gas mixture that serves as the medium for the resonant cavity, and high-purity nitrogen. The high-purity nitrogen must have a purity level of at least 99.99%; otherwise, it may contaminate and damage the lenses within the internal optical path. It is crucial to prioritize gas quality, as failure to do so can easily lead to damage to the laser.
Air Compressors Maintenance
• Check the oil level daily before startup (it should be at the 3/4 mark) and drain any accumulated water after shutdown.
• Clean the cooling grids on both sides (using an air gun) and the air filter on a weekly basis.
• Every 1,000 operating hours, clean the oil and air coolers, and check and adjust the belt tension.
• Every 4,000 operating hours, replace the air filter, oil filter, and compressor oil.
• The operating temperature must not exceed 110°C (under normal operating conditions, it should remain between 80°C and 90°C).
• The electric motor must not be started more than 20 times per hour.
• Do not use the emergency stop button except in an actual emergency.
• The fan blades should rotate counter-clockwise; this indicates that the wiring is correct (i.e., not reversed).
Safety and Security
Fire Protection
Oxygen is needed for the operation of the CNC laser machine, so smoking should be prohibited in the area around the machine, especially near the oxygen cylinder, to prevent hidden dangers and unnecessary damage. (If conditions permit, fire extinguishers should be provided next to the equipment)
Laser Protection
When hitting the center, one must pay attention to make sure the person's hand is away first, turn off the height control (turn off the CLC) and then light. When adjusting the external light path, it must be ensured that no one is standing in the light path range. The operator should also pay attention to ensure that the light will not hit people before lighting. The lighting power and time should be controlled to a reasonable range (the central power is generally 200 between 0.01 and 0.02S. When adjusting the external optical path, the light output power is generally controlled at about 300W, and the light output time is controlled between 0.2 and 0.5S). After the external optical path is adjusted, all protective covers must be installed before cutting. When exchanging air, remove the high voltage first, and close the door immediately after exchanging air. Do not open the door of the electrical cabinet casually, and do not touch the circuits and electronic components inside.
Trends
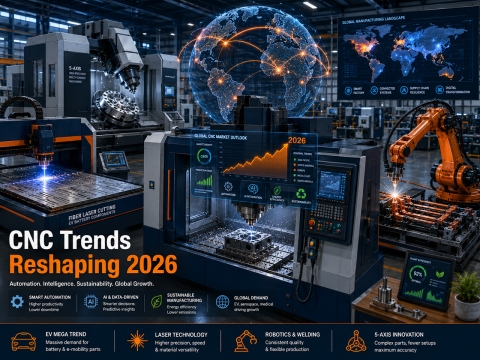
The era of intelligence will come in all respects. Whether it is Germany's Industry 4.0 or China's smart manufacturing, the fourth industrial revolution in the industrial field is quietly coming. As a high-precision laser CNC machine, the laser CNC cutting machine or laser CNC engraving machine is bound to keep pace with the times and fly with technology. The development of laser CNC automation has greatly improved the production capacity and automation level of the workshop.
In the future, on this basis, an era of laser CNC engraving & cutting machines combined with intelligent manufacturing is brewing deeply in the fields of network technology, communication technology, and computer software technology. As an intelligent manufacturing pilot demonstration unit, STYLECNC is relying on its own system technology integration capabilities, focusing on the future development direction and technological commanding heights, and joining strategic partners to build a fully intelligent laser CNC machining factory and create a new situation for intelligent laser CNC engraver and laser CNC cutter.
Start With the Process, Not the Machine
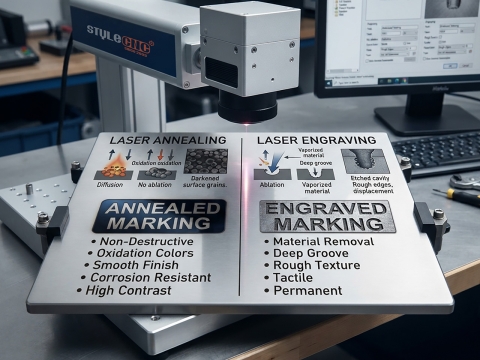
This page gathers five different jobs under one word. Cutting separates parts from sheet, engraving removes material for depth and texture, marking changes the surface without removing much, welding joins metal, and cleaning strips rust and coatings away. Naming the process first cuts the choice down enormously, because a machine built for one rarely does another well. Shops that start from a budget instead of a process usually end up with a machine that does most of what they wanted and none of it excellently. Write down the job, then the material, then the volume, and the category chooses itself.
Wavelength Decides Material, Power Does Not
The single most useful rule on this page is buried in its specification table: three wavelengths are listed, and each suits different materials. A long CO2 wavelength is absorbed by wood, acrylic, leather, and glass, which is why laser cutters for those materials are CO2. The shorter fiber wavelength is absorbed by metal, and ultraviolet is absorbed by plastics and glass so gently that nothing burns. Adding power never changes this: a very strong CO2 laser still will not cut thick steel, and a fiber source still will not cut clear acrylic. Match the wavelength to the material first, then choose power for thickness and speed.
One Pair of Goggles Is Not Enough
Here is a point that catches out shops running more than one laser. Protective eyewear is rated for specific wavelengths, so glasses that block the fiber beam do nothing against a CO2 or ultraviolet one. A workshop with a fiber marker beside a CO2 engraver needs two different pairs, clearly labelled and kept with their machines rather than shared around. Everyone in range of a possible reflection needs them, not only the operator, and the beams from marking machines are invisible, which is precisely what makes casual habits dangerous.
Matching the job to the laser:
| What You Need | Process | Usual Source |
|---|---|---|
| Parts from sheet | Cutting | Fiber for metal, CO2 for organics |
| Text and serial codes | Marking | Fiber, CO2 or UV by material |
| Depth and texture | Engraving | CO2 for wood, fiber for metal |
| Joining metal | Welding | Fiber, handheld or automatic |
| Rust and coating removal | Cleaning | Pulsed or continuous fiber |
Laser buying checklist:
✅ Name the process before comparing machines.
✅ Match wavelength to material, not power to budget.
✅ Buy eyewear rated for each wavelength you own.
✅ Plan extraction and cooling for every laser.
✅ Test your own material before committing.
Things To Consider
This is only a small scratch to know about automatic CNC laser machining. However, by having a basic understanding of these helpful concepts, you'll be able to quickly build upon them and grow your knowledge of CNC laser machine choices.
Frequently Asked Questions
Can one machine cut, mark, weld, and clean?
Handheld three-in-one units genuinely weld, clean, and cut thin metal from one source, which suits repair work. Each function is lighter duty than a dedicated machine, so production volume in any one process still justifies buying for that process.
Do all lasers need a water chiller?
No. Low-power fiber markers are usually air cooled and need nothing more than clear airflow, while CO2 tubes, UV sources, and high-power cutters all rely on clean, temperature-controlled water. Check before planning the installation.
Which lasers need fume extraction?
All of them, though for different reasons. Organics produce smoke, metals produce fine particulate, and coatings produce whatever the coating is made of. Extraction protects lungs and keeps residue off optics, so treat it as part of the machine.
How long does a laser source last?
It depends on the type. Fiber sources are rated around a hundred thousand hours and are replaced as modules, while sealed CO2 glass tubes last thousands of hours and fade gradually. Budget tube replacement as a running cost, not a repair.
Can I add more power later?
Rarely in a useful way. The frame, cooling, and controls are matched to the source, so a meaningful power increase usually means a new machine. Buy for the work you expect within a few years rather than planning to upgrade.
What is a sensible first laser?
For crafts, gifts, and signage, a mid-power CO2 machine covers the widest range of materials cheaply, and an entry laser engraver teaches the fundamentals. For metal fabrication, start with fiber, since no CO2 machine will follow you there.
What Our Customers Say?
Don't take our words as everything. Find out what customers say about our CNC laser machines they have owned or experienced. Why is STYLECNC considered a credible brand and manufacturer to buy a new CNC laser machine? We can talk all day about our quality products, 24/7 excellent customer service and support, as well our 30-day return and refund policy. But wouldn't it be more helpful and relevant for newbies and professionals alike to hear real-life customers experience what it's like to purchase and operate an automatic computer-controlled machine tool from us? We think so too, which is why we've collected tons of genuine feedback to help bring transparency to our unique buying process in-depth. STYLECNC guarantees that all customer reviews are real evaluations from those who have purchased and used our products or services.