Assist gas is one of the largest line items in running a fiber laser, and for many shops it quietly outspends the electricity that powers the beam. That is why the question has shifted from whether air cutting works to how to set it up properly. This guide stays focused on the air side of the decision: how air assist behaves in the kerf, how to size and treat the compressed air, what it does to edge quality, and what it really costs per hour.
How Air Assist Works in the Kerf
Every fiber laser cut needs a gas jet. The beam melts a narrow channel through the sheet, and the coaxial gas stream leaving the nozzle blows the molten metal out of the bottom of the kerf before it can re-solidify. Without that jet, the cut fills in behind the beam.
Air is roughly 78 percent nitrogen and 21 percent oxygen, so it behaves as a blend of the two classic gases. The nitrogen fraction does most of the mechanical ejection work, while the small oxygen share adds a little exothermic energy and leaves a light oxide layer on the cut face. On mild steel and galvanized sheet that oxide is usually cosmetic and paint-ready; on stainless it shows as a faint tint.
Two things made air practical at production scale. Higher-power sources push enough energy into the kerf to cut quickly with a less reactive gas, and shops discovered that the compressor they install is a one-time purchase rather than a monthly invoice. Fabricators who made the switch on high-power fiber laser metal cutting machines often report the most dramatic gas savings, because higher power means faster cutting and less gas per meter.
Which Materials Cut Well with Air
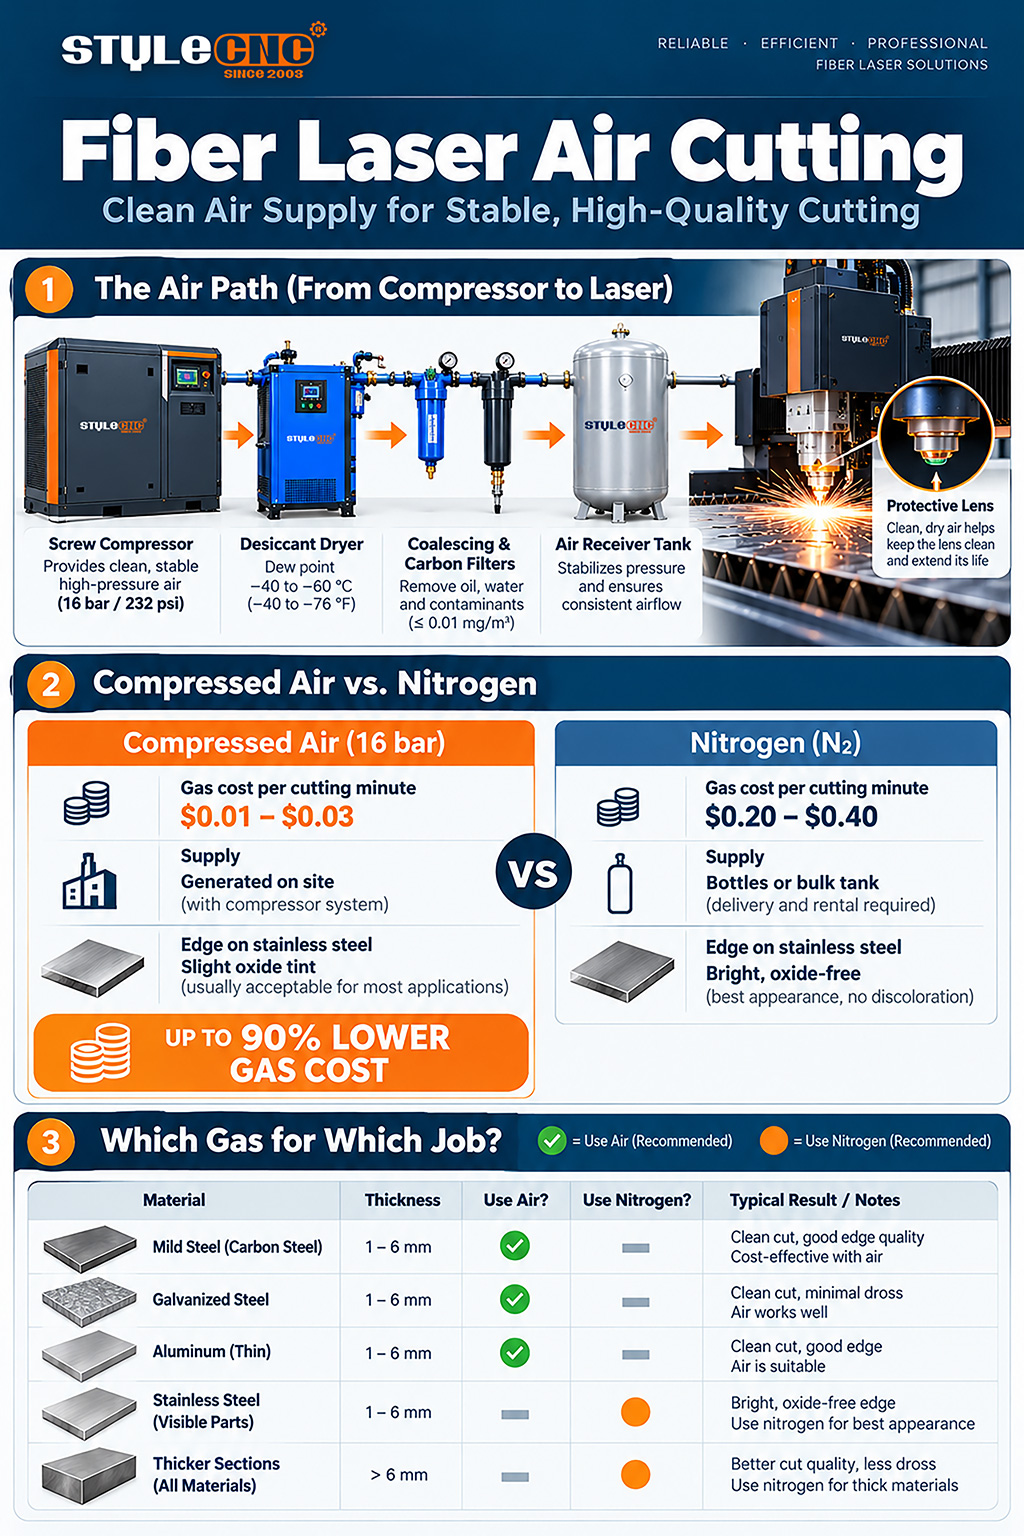
⦿ Mild steel, roughly 1 to 6 mm: a common air window, usually starting around 8 to 12 bar and tuned to the lowest pressure that holds the edge.
⦿ Galvanized sheet: cuts cleanly with air and is one of the strongest use cases for HVAC and enclosure work.
⦿ Thin aluminum: air often performs as well as nitrogen, and several shops report cleaner aluminum edges after switching.
⦿ Stainless steel: cuts fast with air, but expect an oxide tint; acceptable for hidden or painted parts, not for visible brushed finishes.
Operators tend to ask it plainly: will my 3 mm galvanized panels come off the table as clean on air as they do on nitrogen? For most enclosure and ductwork parts the answer is yes. The parts that justify staying on nitrogen are the ones a customer will see, weld without prep, or inspect under bright light. The typical thickness and speed envelopes by source power are mapped in the fiber laser cutting metal thickness, speed, and power guide, which helps set realistic expectations before tuning air parameters.
Compressor Sizing: Pressure, Flow, and Drying
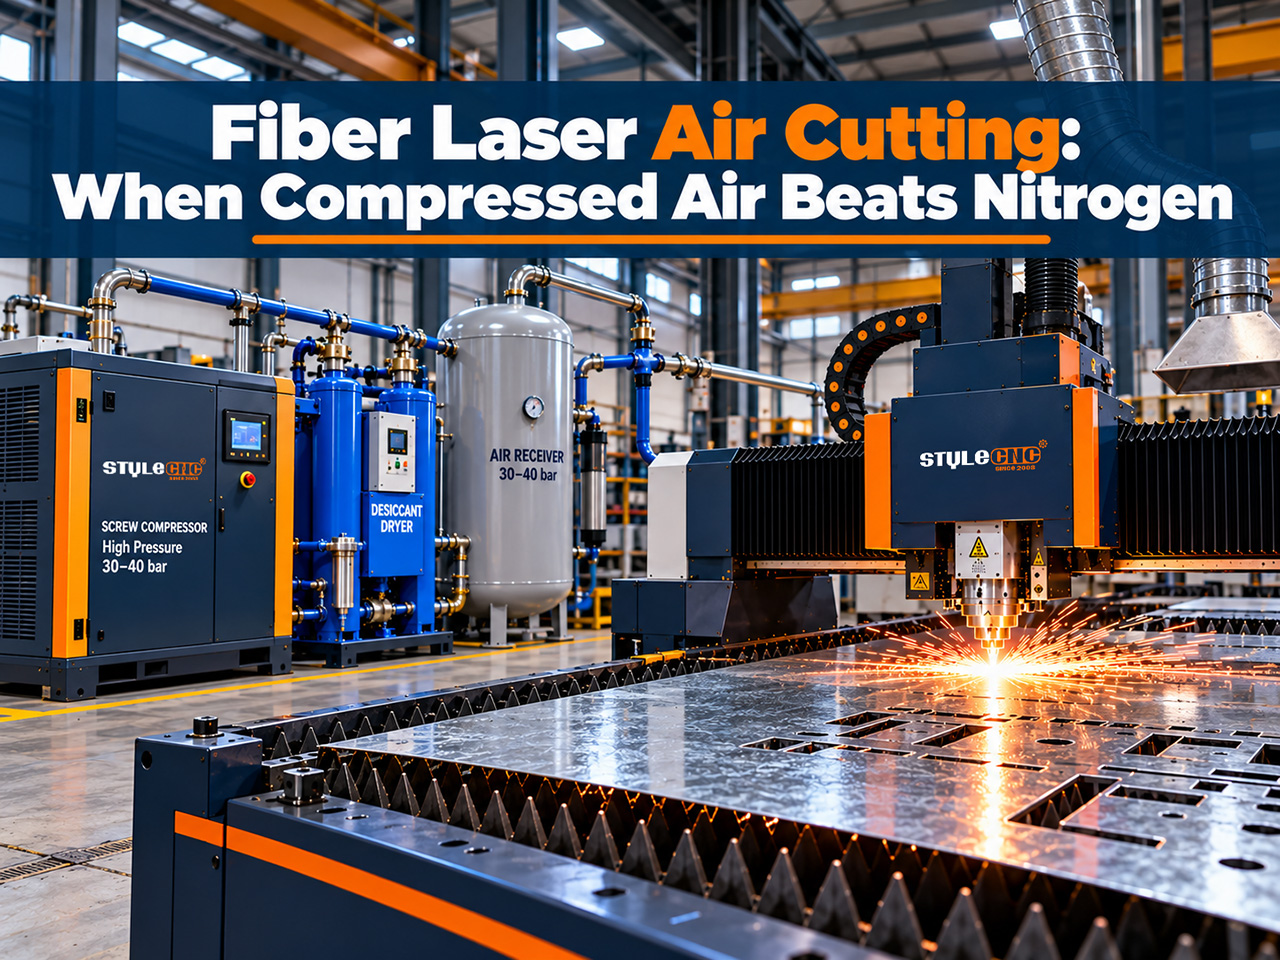
The compressor package decides whether air cutting succeeds. A standard shop compressor running at 7 to 8 bar is built for tools, not for a cutting nozzle, and an undersized system shows up as dross and inconsistent edges long before anyone suspects the air supply.
| Requirement | Typical Target | Why It Matters | Measurement |
|---|---|---|---|
| Delivery pressure | Up to 16 bar class at the machine, 8 to 12 bar common at the nozzle for thin mild steel | Pressure clears molten metal from the kerf; drops cause dross | Gauge pressure at the cutting head during a full nozzle blast |
| Free air delivery | Matched to nozzle and power; roughly 0.5 m³/min consumption on mid-power work | Undersized flow starves long cuts and large nozzles | Measured consumption against rated delivery at working pressure |
| Dryness | Pressure dew point of minus 40 to minus 60 °C | Moisture fogs and cracks the protective lens | Dew point reading downstream of the dryer |
| Oil and particles | Oil-free or oil removed by coalescing and carbon filtration | Oil vapor burns onto optics and contaminates edges | Filter differential pressure and lens inspection interval |
| Buffer storage | Receiver tank sized to absorb demand spikes | Laser controllers dislike pressure fluctuation | Pressure swing during piercing and rapid contour changes |
Pressure and flow
Specify the compressor at the pressure the nozzle needs plus the losses through dryers, filters, and piping. Flow comes from nozzle diameter and how many minutes per hour the beam is on. As a reference point, one published setup pairs a 16 bar compressor delivering about 1.27 m³/min from 13.4 kW of input power with an actual cutting consumption near 0.5 m³/min, leaving headroom for piercing and larger nozzles.
Drying and filtration
This is the step shops skip and later regret. Compressed air carries moisture and oil vapor, and both end up on the protective lens in the cutting head. A fogged or contaminated lens scatters the beam, weakens the cut, and can crack under heat. Air treatment suppliers typically specify a pressure dew point between minus 40 and minus 60 °C, which means a desiccant or high-performance dryer after the compressor, followed by coalescing and activated carbon filters. Understanding where the protective lens sits in the head, covered in the guide to fiber laser cutting machine main parts, makes it obvious why air quality protects the most expensive consumable in the system.
Piping, placement, and maintenance
Place the compressor close to the laser so the high-pressure run is short, and use piping rated for the full working pressure rather than ordinary shop lines. Every elbow, quick coupler, and long hose run costs pressure at the nozzle, which is why many installs dedicate a separate high-pressure line to the cutting head while a regulator feeds lower-pressure air to the rest of the workshop.
Treat the air package as part of the laser, not as building services. Drain the receiver and check the auto drains daily, log dew point weekly, and change filter elements on differential pressure rather than on guesswork. A single wet morning after a skipped drain can cost more in protective lenses than a year of filter elements.
Edge Quality Trade-Offs
Air cutting is not a free swap; it is a deliberate trade between gas cost and edge appearance. Industry case reports put air-cut edge quality close to oxygen or nitrogen on many parts, but the difference that remains is predictable:
⦿ Mild steel: light oxide on the cut face, typically fine for painting and powder coating after normal pretreatment.
⦿ Stainless: faint yellow to grey tint and a less bright face than nitrogen; may need cleaning before welding or polishing.
⦿ Aluminum: often equal to or better than nitrogen on thin sheet, with low dross when pressure is tuned.
⦿ Thicker sections: dross risk rises as thickness climbs, which is where nitrogen or oxygen usually returns to the program.
Piercing deserves its own note. Many air setups pierce at lower pressure and then step up for the cut, because a full-pressure blast during piercing can splash molten metal back toward the nozzle. Let the controller manage that pressure switch rather than running one fixed value through the whole contour.
The practical rule is to sort the order book by what the customer sees. Hidden brackets, painted panels, and steel fabrication parts bound for coating are ideal air candidates. Architectural stainless and food-grade parts generally stay on nitrogen, and keeping both gases piped to the laser cutter machine lets the cutting program choose per job.
Switching usually means retuning, not just swapping a gas line. Expect to adjust nozzle size, focus position, and pressure on each material and thickness, then save the air parameters as their own cutting library. Most shops run test coupons for a week on scrap before moving live jobs across, and that week tends to answer the edge quality question better than any spec sheet.
Cost per Hour Compared with Nitrogen
Gas cost scales with beam-on time, nozzle size, and pressure, and nitrogen cost rises steeply with every extra bar. Air changes the structure of the bill: instead of paying per cubic meter delivered, the shop pays once for the compressor and then mainly for the electricity to run it. On a two-shift operation, that difference compounds quickly.
| Factor | Compressed Air | Nitrogen | Measurement |
|---|---|---|---|
| Gas cost per cutting minute | About $0.01 to $0.03, mostly electricity | About $0.20 to $0.40, higher at high pressure | Gas spend divided by beam-on minutes |
| Cost per cubic meter | Baseline | At least three times air, above ten times in some regions | Delivered price per m³ including rental and delivery |
| Supply logistics | Generated on site, on demand | Bottles, dewars, or bulk tank with boil-off losses | Downtime hours waiting on gas delivery |
| Upfront investment | High-pressure compressor, dryer, filters, receiver | Tank rental or generator, plus ongoing gas | Payback months on the air package |
| Edge result on stainless | Slight oxide tint at the edge | Bright, oxide-free edge | Whether the part needs post-cut cleaning |
The case studies make the numbers concrete:
⦿ One Australian fabricator spending over $9,000 a month on bottled nitrogen installed a 22 kW, 16 bar compressor package and reported about $96,000 in annual savings, even after running and service costs.
⦿ A tray manufacturer reported roughly $42,000 a year in savings, with the compressed air system paying for itself within a year.
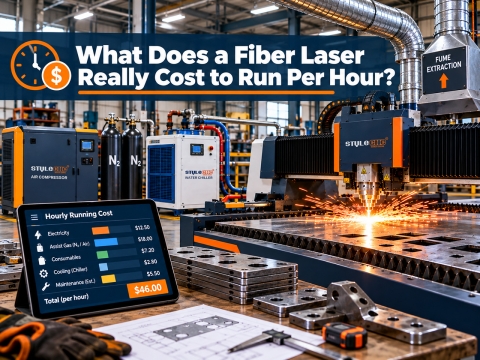
⦿ A US contract manufacturer brought fiber laser running cost below $4 per hour, about 90 percent cheaper than its nitrogen baseline, while cutting most of its stainless work on shop air.
Your own payback calculation needs three numbers: current monthly nitrogen spend, beam-on hours per month, and the installed price of a correctly sized compressor and treatment package. Subtract the compressor's electricity and service cost from the nitrogen bill, and the remaining figure tells you how many months the package takes to pay for itself. Shops cutting mostly coated mild steel and aluminum parts tend to see the fastest returns, because the oxide trade-off costs them nothing.
Pre-Switch Checklist
✔ Pull twelve months of nitrogen invoices, including tank rental and delivery charges.
✔ Sort the part mix into visible stainless, coated steel, galvanized, and aluminum, and estimate the share air can take.
✔ Specify the compressor for nozzle pressure plus line losses, with flow matched to your largest nozzle.
✔ Budget the dryer, coalescing and carbon filters, and receiver tank as part of the package, not as extras.
✔ Keep nitrogen available for visible stainless and thick sections, and let the cutting program select gas per job.
Configure Your Fiber Laser for Air Cutting
Compare power levels and bed sizes across the full range of fiber laser cutting machines, and request a free quote that includes a matched high-pressure compressor and air treatment package for your materials.