Most new laser owners underprice their first year. They quote the beam-on time, forget the pierces, the setup, the scrap skeleton, and the hour spent answering emails, and then wonder why a busy machine is not paying its lease. This guide gives you a pricing formula you can defend, shows where each pricing model works and fails, and runs a full break-even calculation so the numbers on your quotes trace back to real costs.
The Core Pricing Formula
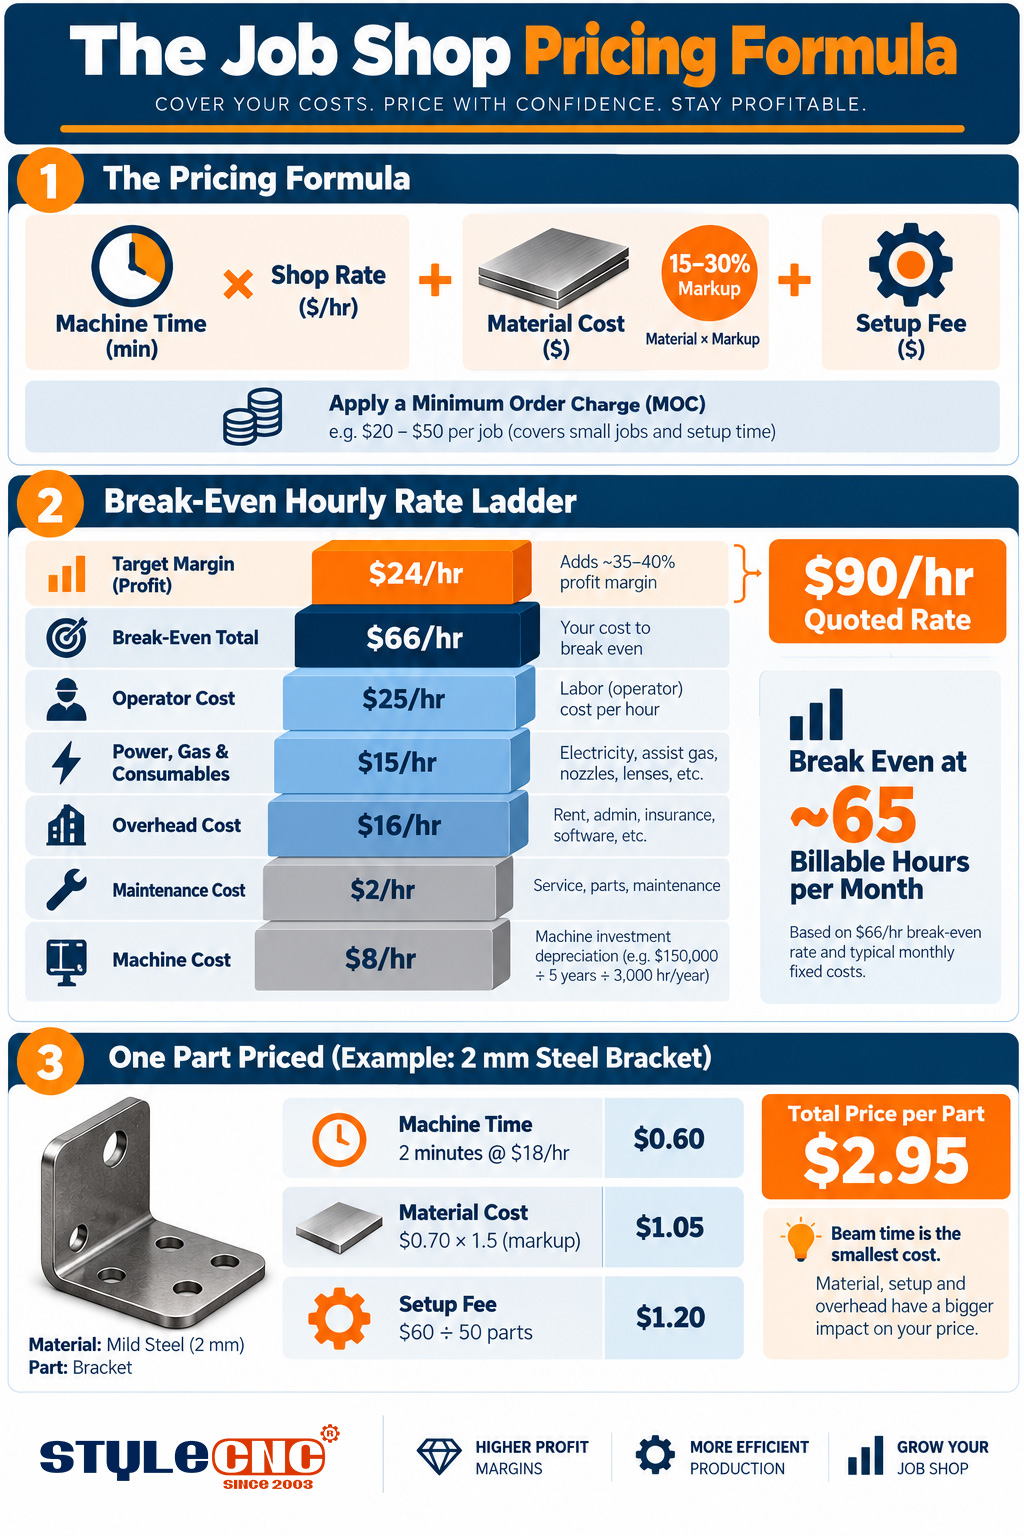
Every sound metal cutting quote reduces to four parts:
⦿ Machine time: cutting time plus piercing time from the nesting software, multiplied by your machine hour rate.
⦿ Material: the share of the sheet the part consumes, including its portion of the skeleton, with a markup applied.
⦿ Setup: programming, nesting, file cleanup, and loading, charged once per job and spread across the quantity.
⦿ Secondary work: deburring, bending, tapping, or finishing, priced separately so the cutting rate stays clean.
Industry pricing guides describe the same structure: cut time multiplied by an hourly rate, plus setup, material, and finishing. What separates profitable shops is not the formula; it is the accuracy of the shop rate they plug into it. If you are still mapping out the business itself, the guide on how to start your business with a laser cutter covers the wider setup decisions this pricing model sits inside.
Be honest about billable hours
The denominator in your shop rate is where optimism does the most damage. A year has roughly 2,000 single-shift hours, but changeovers, maintenance, quiet weeks, and programming time mean few small shops bill anywhere near that. Starting with 1,200 to 1,500 billable hours for a single shift gives a rate that survives a slow month; you can lower it once your records prove higher utilization.
Pricing Models: Per Part, Per Inch, and Machine Hour
Shops present prices in different ways, but every model should be derived from the same underlying cost per machine hour:
| Pricing Model | How It Works | Where It Breaks Down | Measurement |
|---|---|---|---|
| Per part | One price per piece, built from machine time, material, and setup | Needs a solid cost model behind it or margins drift | Quoted price against actual cost per part |
| Per inch or per meter | Rate applied to total cut path length | Ignores pierce count, thickness, and material cost | Pierces per part and sheet thickness |
| Machine hour | Nest run time multiplied by an hourly rate, plus material | Customers struggle to compare it with per-part quotes | Beam-on minutes from the nesting software |
| Per sheet | Flat price to cut a full nested sheet | Rewards dense nests, punishes sparse ones | Sheet utilization percentage |
Why per-inch pricing misleads on metal
Customers often ask for a laser cutting price per inch, so it helps to know why the number is slippery. A fiber laser cuts thin mild steel at several meters per minute, so the beam time for an inch of cut can be fractions of a cent. On thin sheet, the pierces, setup, and material dominate the cost, not the length of cut.
Thickness flips that relationship, because cutting speed falls steeply as the plate gets heavier. The same per-inch rate that overcharges on 1 mm sheet loses money on 12 mm plate. If you must quote per inch, keep separate rates by material and thickness band, and add a per-pierce charge. The fiber laser cutting thickness, speed, and power reference shows how sharply speed changes across thicknesses, which is exactly what a flat per-inch rate ignores.
Material and gas surcharges
Not every laser metal cutter costs the same per hour. Stainless and aluminum cut on high-pressure nitrogen carry a gas cost that mild steel on air or oxygen does not, and thick plate wears nozzles and protective lenses faster. Many shops keep one base rate and add a surcharge per hour for nitrogen work and heavy plate, which keeps quotes simple without hiding real costs.
Material Markup
Material is the line new shops most often give away. Charging the customer exactly what you paid for the sheet means you carry the cost of buying it, storing it, handling it, and scrapping the skeleton for free.
⦿ Charge for the material consumed, including the part’s share of the skeleton, not just the part’s net area.
⦿ Apply a markup to cover purchasing, storage, handling, and the remnants you never sell; many shops work in the 15 to 30 percent range.
⦿ Reprice stock regularly; steel and aluminum move, and a quote built on last quarter’s invoice can erase the margin on a large job.
⦿ When customers supply their own material, raise your machine rate or add a handling fee, because you still own the scrap risk.
Remnants deserve a policy too. Either price them into the markup and treat any later reuse as a bonus, or track usable offcuts by size and credit them on future jobs. Shops that do neither quietly pay for the same steel twice.
Minimum Order Charges
A minimum charge protects you from the job that costs more to process than it earns. A single small bracket still needs a quote, a file check, a nest, a sheet loaded, and an invoice raised. Without a minimum, that one-part order can take half an hour of staff time for a few dollars of revenue.
Set the minimum at roughly the cost of one setup plus a short machine slot at your shop rate. Owners on fabrication forums commonly describe minimums that land somewhere between the cost of 30 minutes and one hour of machine time. Show it clearly on your price list so customers can batch small orders instead of being surprised at invoice time.
Break-Even Worked Example
The table below uses round illustrative numbers for a small single-machine shop running 1,500 billable hours a year. Replace each line with your own figures; the method matters more than these values.
| Cost Line (illustrative shop) | Amount | Per Billable Hour (1,500 h/yr) |
|---|---|---|
| Machine cost spread over 5 years ($60,000) | $12,000 / yr | $8.00 |
| Maintenance, lenses, nozzles, service | $3,000 / yr | $2.00 |
| Rent, insurance, software, admin overhead | $24,000 / yr | $16.00 |
| Power, assist gas, consumables while cutting | Variable | $15.00 |
| Operator, fully loaded | Variable | $25.00 |
| Break-even machine rate | $66.00 | |
| Rate with 30 percent margin (rounded) | $90.00 |
Fixed costs here total $39,000 a year, or about $3,250 a month. At a $90 rate, each billable hour contributes $50 after variable costs, so the shop breaks even at roughly 65 billable hours a month. Every hour beyond that is profit, which is why utilization, not the headline rate, decides whether a laser business is profitable.
Turning the rate into a part price
Take a 2 mm mild steel bracket with a 1,200 mm cut path and eight pierces, ordered in a batch of 50. Including acceleration in corners and the pierces, assume about 24 seconds of machine time, or $0.60 at $90 an hour. The blank and its skeleton share weigh about 0.7 kg; at roughly $1.20 per kilogram with a 25 percent markup, material adds about $1.05. A $60 setup spread across 50 parts adds $1.20.
That puts the cost-based price near $2.85, quoted at $2.95 per part, or $147.50 for the batch, comfortably above a typical minimum. Notice that the beam time is the smallest of the three lines. Order 500 instead of 50 and the setup share falls to $0.12, which is the honest basis for a volume discount. The cost of buying the equipment in the first place, covered in how much a laser cutting machine costs, is what sets the depreciation line in your own version of this table.
Volume discounts that do not cost you
Discount only what volume actually saves. Setup spreads thinner, nesting gets denser, and material buys get cheaper as quantity grows, so those lines can fall. Machine time per part does not, so the rate itself should stay put. Publishing quantity breaks at 10, 50, and 250 pieces shows customers the savings while keeping every tier above your break-even.
Is a Metal Laser Cutting Business Profitable?
It can be, provided three conditions hold. The shop rate must be built from real costs, the machine must be busy enough to clear fixed costs comfortably, and the shop must win work on lead time and reliability rather than price alone.
Forum discussions among job shop owners point the same way: operators running older, slower machines describe high hourly rates and thin demand, while shops with modern fiber equipment face a more competitive market where speed lowers the cost of every part. A faster sheet metal laser cutter does not just cut more parts; it lowers your break-even rate, which gives you room to compete on price while keeping margin. Browsing finished laser cutting projects is also a practical way to spot part types and markets local competitors are underserving.
Quoting speed is the other quiet profit lever. Buyers sending the same drawings to three shops often order from whichever replies first with a clear price. A spreadsheet or quoting tool built on the formula above lets you return a defensible number within the hour, and fast, consistent quotes win repeat work more reliably than undercutting.
Quoting Checklist
⦿ Build your machine hour rate from fixed costs, variable costs, and realistic billable hours, then add margin.
⦿ Take cut time and pierce count from the nesting software, never from a guess.
⦿ Charge material by sheet share including the skeleton, with a markup, and reprice stock regularly.
⦿ Add a setup fee per job and a published minimum order charge.
⦿ Price secondary operations separately and review actual job costs monthly against quotes.
Lower Your Break-Even Rate with the Right Machine
Faster cutting means a lower cost per part and more room on every quote. Compare power levels and bed sizes across the range of fiber laser cutting machines and get a free quote matched to your materials and target workload.