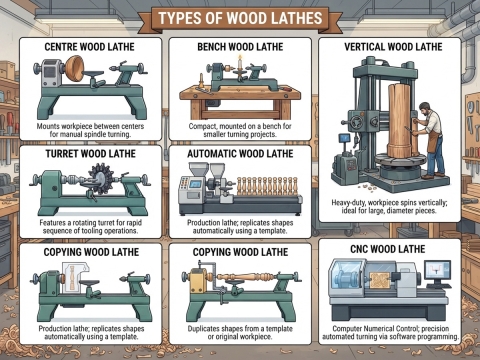
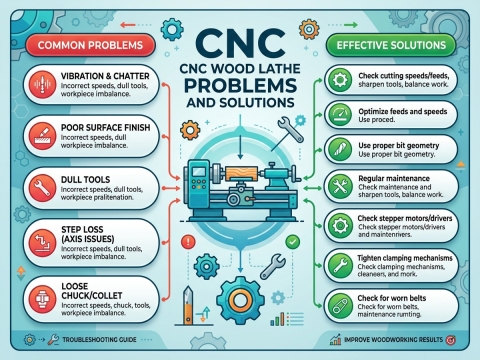
A wood lathe is a machine tool that uses woodturning tools to shape the surface of wood or create complex profiles.
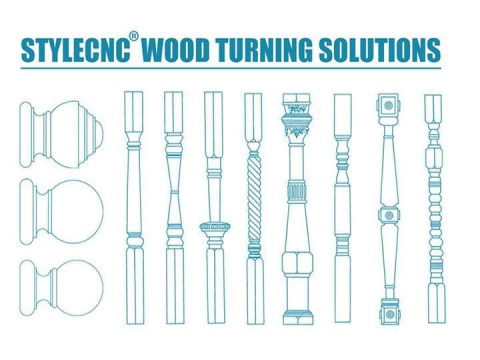
Wood lathes are primarily used to manufacture items such as staircase balusters, Roman columns, table and chair legs, washbasins, wooden vases, wooden-column tables, dowels, furniture components, and crib posts. They are also capable of producing plates, goblets, bottle caps, handles, rolling pins, flutes, and cello accessories. CNC wood lathes are particularly well-suited for batch production in small and medium-sized woodworking enterprises, offering the flexibility to define shapes and rapidly switch between machining styles. Unlike traditional lathes, which are limited to processing a single workpiece at a time, CNC wood lathes (including dual-axis and three-axis models) can simultaneously process two or three identical workpieces. The equipment is user-friendly, featuring intuitive design software and one-touch style switching, allowing operators without specialized backgrounds to become proficient after brief training. Fully automated CNC wood lathes enable a single operator to manage two or three machines simultaneously, thereby significantly boosting production efficiency, reducing labor and costs, and delivering substantial economic benefits.
Instructions
❇️ Check that the turning tool is securely fastened. Verify the status of the power supply, air supply, and machining area, and ensure the workpiece is firmly clamped.
❇️ Before machining, confirm that the program input is correct, the tool offset is accurate, and system parameters are properly set.
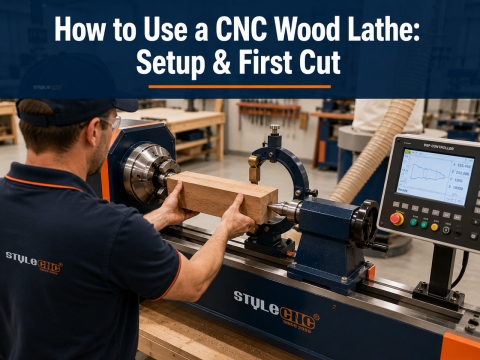
❇️ Turn the selector switch to "Auto" mode, select the desired machining program, and press the "Cycle Start" button.
❇️ The machine will begin returning to the mechanical home position to prepare for machining.
❇️ Press the "Cycle Start" button to begin operation; the spindle will start rotating (if the tool turret begins to feed but the spindle does not rotate, press the "Start" button). Spindle speed adjustment: Adjust based on workpiece material, machining geometry, and tool type; generally, hard materials require higher speeds, while standard speeds suffice for soft materials. If vibration occurs during machining, adjust the speed to eliminate it.
❇️ Upon completion of machining, the system will automatically return to the initial position.
❇️ To machine a new workpiece, simply press the "Cycle Start" button again; to switch programs, repeat the steps above.
❇️ To exit the machining program, press the "Exit" button or turn the selector switch to the "Setup" position; the system will return to the initial interface.
❇️ If any abnormality is detected during machining, press the "Emergency Stop" button to halt all operations. To pause briefly for inspection, press the "Pause" button; press it again to resume machining.
Note: Use a low feed rate during machining. "Rapid traverse" speeds may be used for tool retraction or non-cutting movements. Rapid feed rates are suitable for smooth, continuous sections, while speeds should be reduced in areas with drastic diameter changes. For sections with sudden or significant diameter variations, it is recommended to machine the larger diameter section first, followed by the smaller diameter section at a lower speed.
Precautions
⛔ Do not install the equipment during thunderstorms; do not install power outlets in damp locations; never touch uninsulated power cables.
⛔ Operators must undergo rigorous training; prioritize personal and equipment safety during operation and strictly adhere to operating procedures when using the CNC wood lathe.
⛔ The required power supply voltage is 220V or 380V, with a fluctuation range of less than 5%. If the voltage is unstable or high-power equipment is nearby, select a voltage stabilizer under the guidance of a professional technician.
⛔ The CNC wood lathe and control cabinet must be reliably grounded. Connecting or disconnecting data cables while the power is on is strictly prohibited.
⛔ Operators are strictly prohibited from wearing gloves while working; the use of safety glasses is recommended.
⛔ The machine body is made of castings, which are relatively brittle; apply moderate force when installing screws to avoid stripping the threads.
⛔ Cutting tools must be installed and clamped correctly, and kept sharp. Dull tools reduce turning quality and can cause motor overload.
⛔ Do not place fingers in the tool's working area; dismantling the turning head for other purposes is strictly prohibited. Processing materials containing asbestos is strictly prohibited.
⛔ Do not exceed the machine's specified processing limits. Disconnect the power supply when the machine is not in use for extended periods. Machine relocation must be performed under the guidance of professionals.
⛔ If the machine malfunctions, consult the troubleshooting section of the operation manual or contact the dealer to avoid personal injury or equipment damage.
Safety Rules
⚠️ Before operating the CNC wood lathe, securely mount the workpiece, tighten the tailstock locking nut, and lock the tailstock center using the locking mechanism. Rotate the workpiece by hand to check its condition and adjust the tool rest position. The gap between the tool rest and the workpiece should be maintained at 2–3 mm. If the gap is too wide, the tool may dig into the wood ("tool digging"), potentially causing a safety accident.
⚠️ After clamping the wood, manually rotate the chuck to verify alignment and check that the tool shank screws and the tool rest are securely fastened; proceed to connect the power and run a test only after confirming everything is correct.
⚠️ For workpieces longer than 100 mm, the tailstock center must be used to hold the workpiece firmly in place.
⚠️ When installing the turning tool, the length of the tool shank extending from the tool rest should be less than 50 mm, and the total shank length should be approximately 150 mm. When machining large workpieces (diameter over 500 mm), the tool must be securely fastened to the tool rest, and the cutting edge should not be excessively sharp.
⚠️ Set appropriate cutting parameters. During rough turning, reduce the depth of cut to account for the workpiece's angular edges. Once the edges are turned down and the workpiece is roughly shaped, the rotational speed can be increased for subsequent processing.
⚠️ Keep the cutting edge sharp. Using a dull tool not only compromises machining quality but also increases the risk of accidents.
⚠️ Do not cut small workpieces containing knots. Avoid high-speed feed rates when machining workpieces with knots; remove any hard foreign objects from the wood before processing.
⚠️ When turning irregular, angular wood stock, first use a stationary tool to cut away the sharp edges before proceeding to finish turning.
⚠️ Use sandpaper to smooth the surface of the turned part for a better finish. Don't apply excessive pressure during sanding. Move the sandpaper at a steady speed along the workpiece surface to achieve the desired finish while avoiding excessive wear on the workpiece.
⚠️ Use a low feed rate for the initial cut on the CNC wood lathe. When sanding with abrasive cloth or sandpaper, position your right hand in front and your left hand behind, applying even pressure.
⚠️ Glued wood assemblies must be allowed to set for 24 hours before turning.
⚠️ The rotational speed of the lathe machine depends on the dimensions and material of the workpiece.
⚠️ Select an appropriate spindle speed: reduce the speed when turning large workpieces, as high rotational inertia can lead to accidents; conversely, the speed can be increased for smaller workpieces to achieve a smoother surface finish. Crucially, before turning a raw workpiece, the wood blank must be rounded off. Turning square stock directly is strictly prohibited, as it poses a significant safety risk.
⚠️ Strictly adhere to the safety operating procedures for the lathe machine. Inspect all components to ensure they are functioning correctly before starting the machine.
Maintenance Rules
CNC wood lathes require inspection and maintenance both before and after operation. Specific maintenance guidelines are as follows:
*️⃣ Lathe Lubrication: To ensure proper operation, minimize wear, and extend service life, all friction points on the lathe must be lubricated, and daily maintenance must be prioritized.
*️⃣ Oil Pump Lubrication: A continuous, forced lubrication mechanism typically used for high-speed components requiring large volumes of lubricant. This method is employed at multiple lubrication points within the headstock.
*️⃣ Common Lathe Lubrication Methods: Lathes utilize various lubrication forms; common methods include:
✓ Oil Pouring/Dripping: Typically used for exposed sliding surfaces, such as the bedways.
✓ Splash Lubrication: Typically used for enclosed housings. For example, as gears within the headstock rotate, they splash lubricant from the bottom of the housing into an upper oil trough; the oil then flows through holes in the trough to various lubrication points.
✓ Oil Wick Lubrication: Typically used for oil reservoirs in feed boxes or apron assemblies. This method utilizes the oil-absorbing and wicking properties of oil lines (or ropes) to guide lubricant to specific points, providing intermittent drip lubrication.
✓ Ball-Check Oil Cup Lubrication: Typically used for components such as tailstock bearings, carriage handwheels, and supports for lead screws, feed rods, or control levers. Oil is injected by pressing an oil gun against the ball at the top of the cup; once the gun is removed, the ball resets and seals the opening, preventing dust ingress.
✓ Grease Cup: Typically used for components such as change-gear boxes, gear bracket shafts, or areas where frequent lubrication is inconvenient. The cup is pre-filled with calcium-based grease; when lubrication is required, tightening the cup lid forces the grease toward the lubrication point.
Proper maintenance as described above makes the CNC wood lathe easier to operate and extends its service life.